The short answer
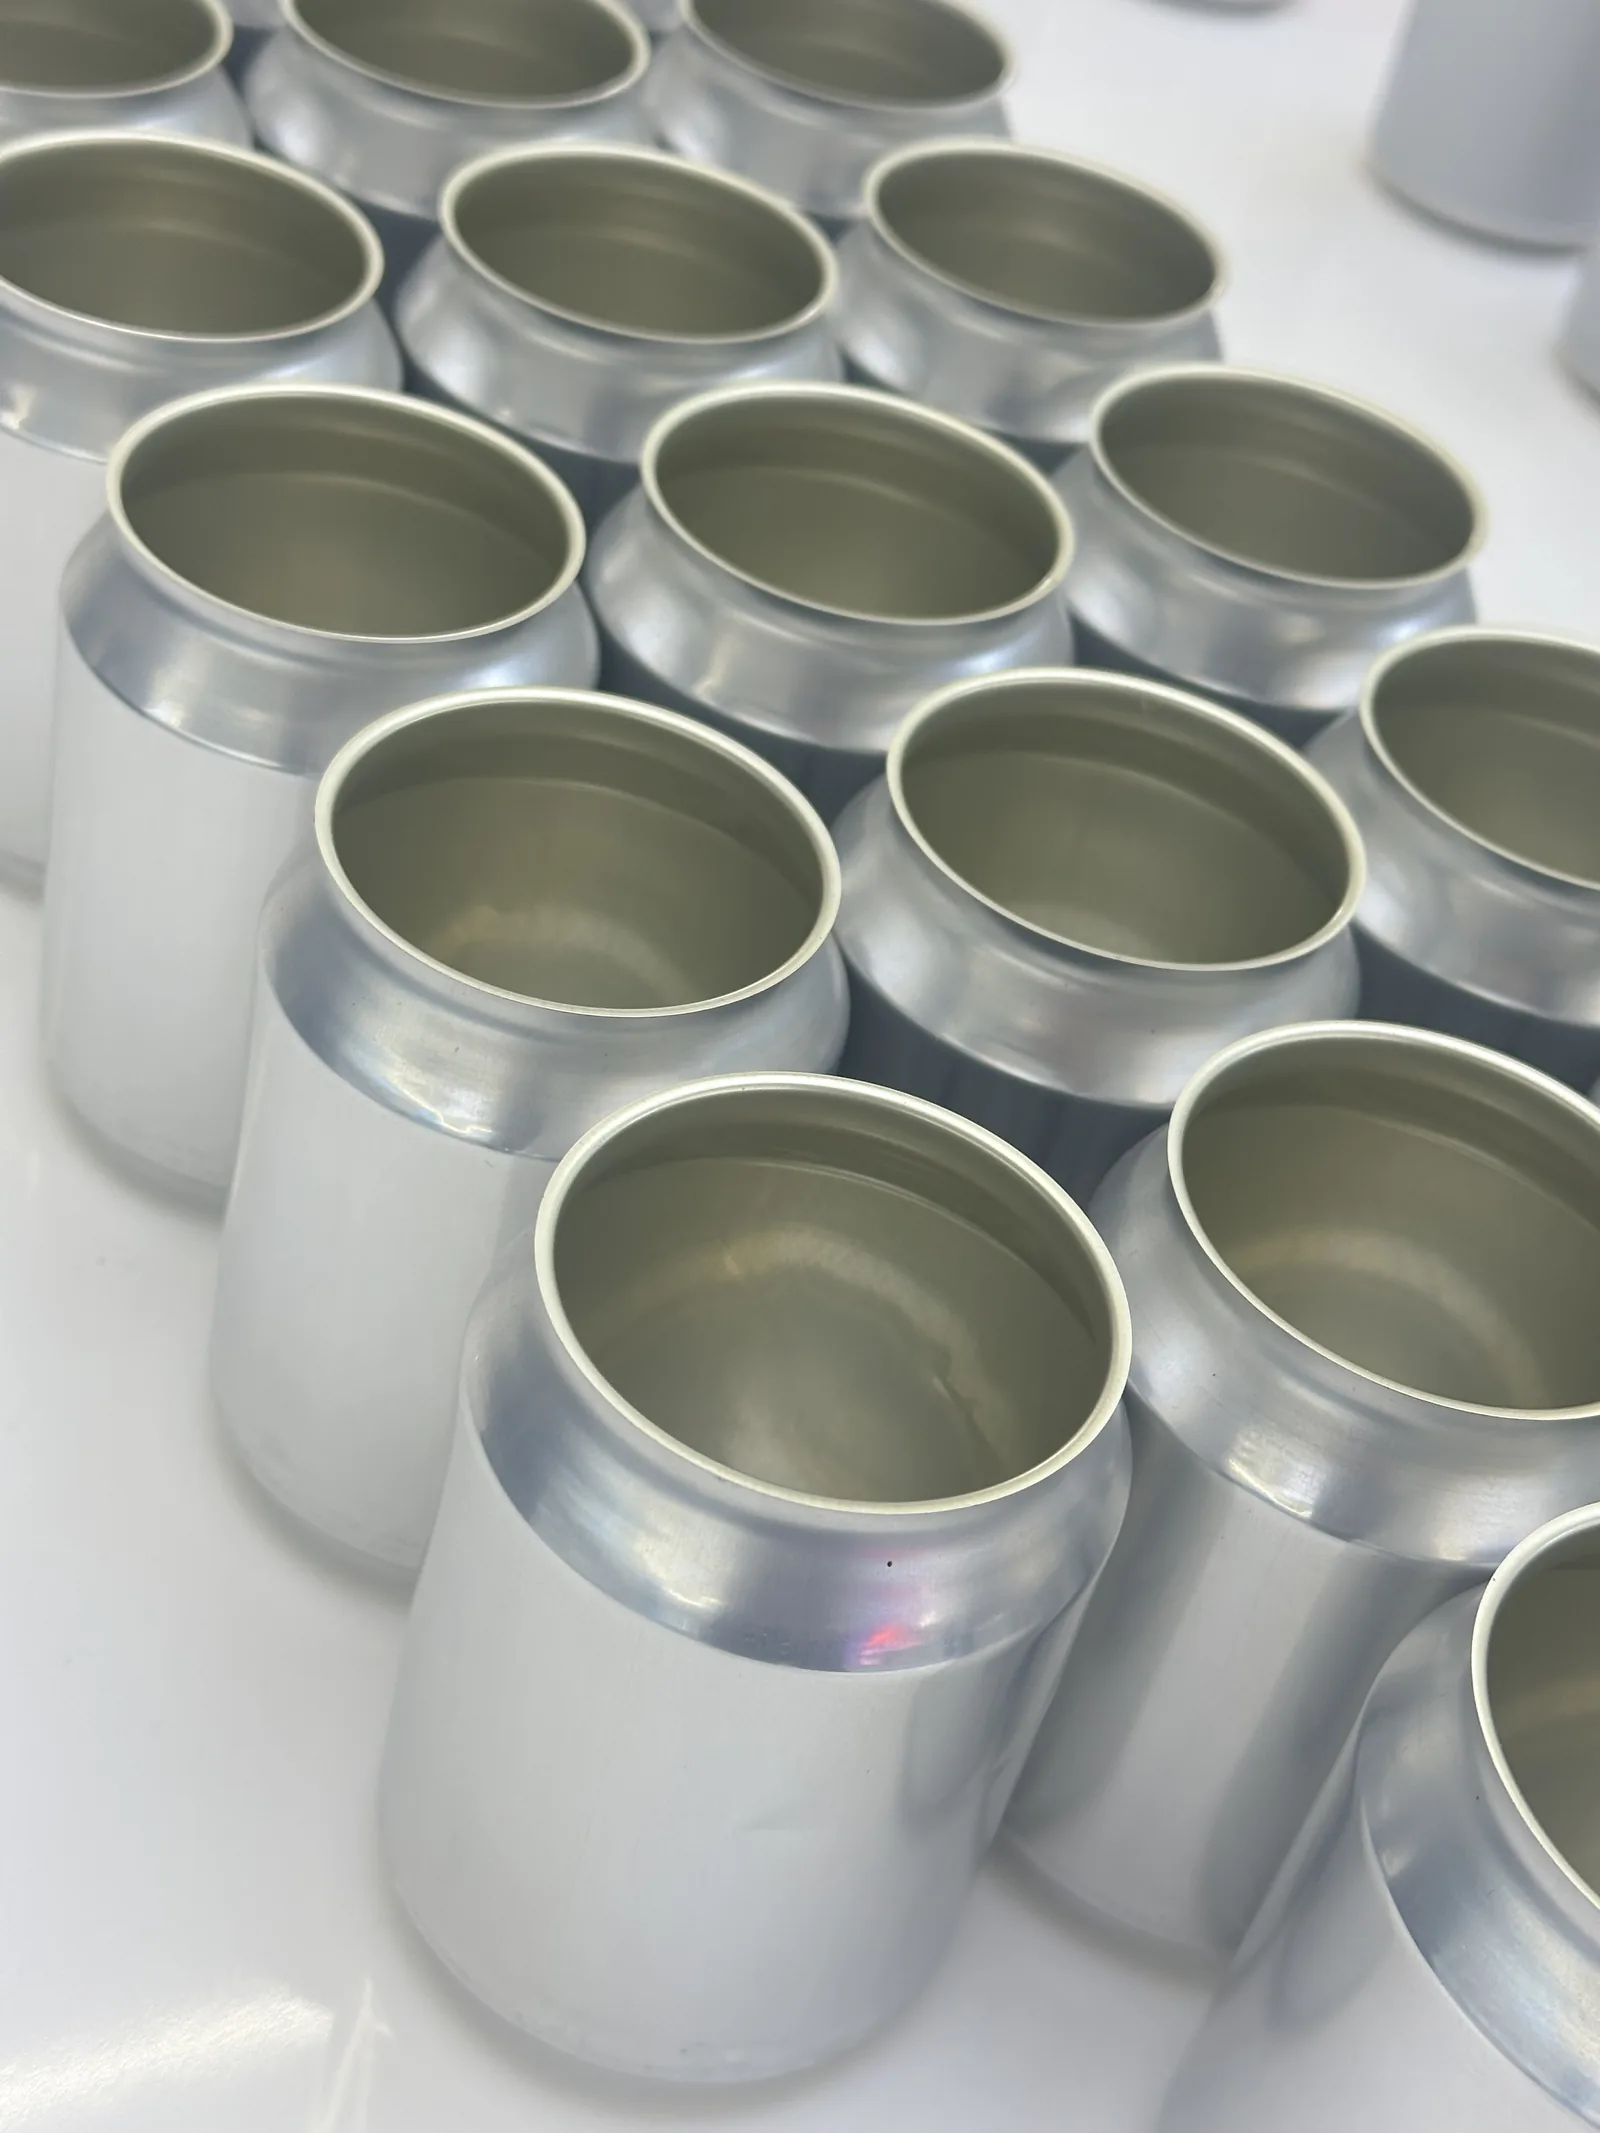
Choose 3104 or 3004 aluminum can body stock against the specification for your two-piece draw-and-iron (D&I) line. If your customer already specifies an alloy, keep it unless the customer approves a change. For a new specification, agree on the temper, thickness and tolerances first, then qualify the candidate coil on your line.
Composition: 3104 vs 3004
Both are 3xxx series, aluminum-manganese-magnesium, and on paper their registered compositions sit close together.
| Element (wt%, max unless a range is shown) | 3104 | 3004 |
|---|---|---|
| Silicon (Si) | ≤ 0.60 | ≤ 0.30 |
| Iron (Fe) | ≤ 0.80 | ≤ 0.70 |
| Copper (Cu) | 0.05–0.25 | ≤ 0.25 |
| Manganese (Mn) | 0.8–1.4 | 1.0–1.5 |
| Magnesium (Mg) | 0.8–1.3 | 0.8–1.3 |
Registered composition limits per EN 573-3 / GB/T 3190.
Both alloys have the same registered magnesium range, and their manganese ranges overlap. 3104 has higher registered silicon and iron limits and a specified copper minimum. These are composition limits; qualifying the coil still requires the agreed mechanical properties and forming checks.
Qualify the coil on your line
For either alloy, confirm the temper and thickness with the buyer. Compare the material specification with what your cupper, bodymaker and downstream equipment require. Agree on the acceptance criteria for earing, surface finish and ironing before qualifying a coil.
If your line already runs an approved 3104 or 3004 material, use that qualified specification. For a new line or material change, review the candidate alloy, temper and thickness together, and confirm the choice through your qualification process.
Before you order: four checks
- Read your specification first. If it names an alloy, a temper, and a gauge range, the question is already answered. Don’t switch alloys without your customer’s approval.
- Match the temper to the process. D&I can body stock is typically H19. H19 and O aren’t interchangeable. If your process was qualified on a different temper, tell us before production so the temper gets agreed against your spec.
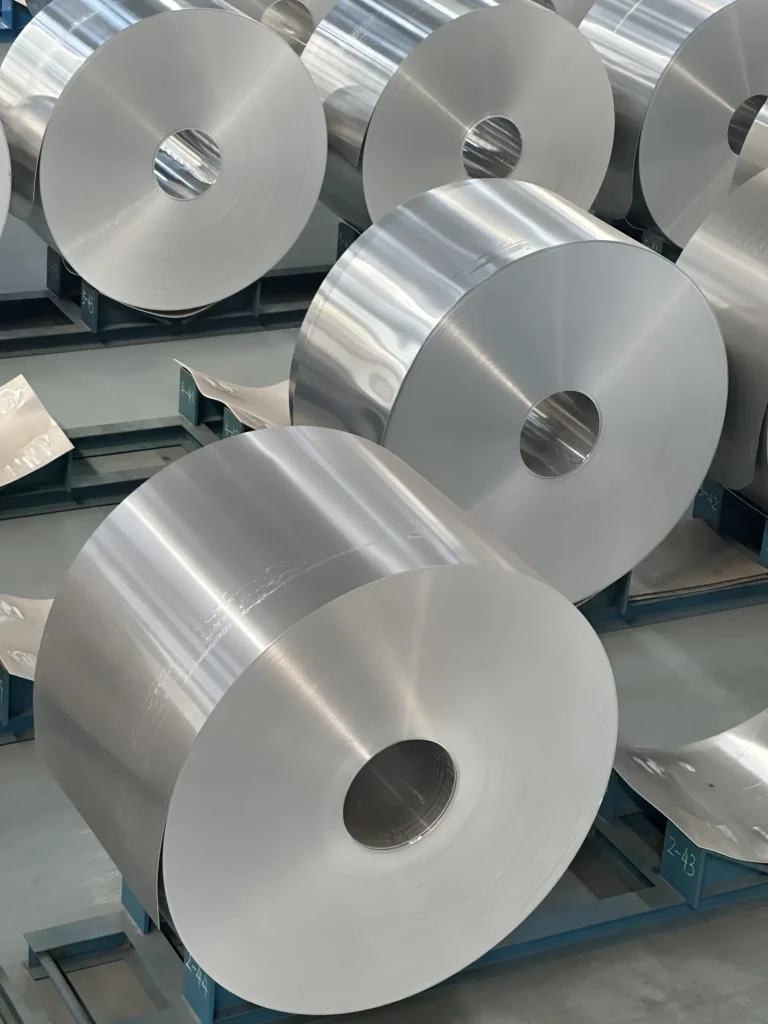
- Confirm gauge and width together. Our standard 3104 coil runs 0.2–3.0 mm, custom gauges on request. The plant’s overall cold-rolled capability covers 0.2–3.8 mm, finishing width 1200–2150 mm, hot-rolled width 1150–2150 mm. Those are overall capabilities, not a promise that every combination exists. Confirm alloy, temper, gauge, width, tolerance, and coil weight for your order, and check both against your cupper and your coil handling.
- Ask for the paperwork with the coil. Our factory is ISO 9001, ISO 14001 and ISO 45001 certified. Confirm mill certificate availability, test items, and format when you enquire.
Frequently asked questions
What thickness of 3104 do I need for can body stock?
Depends on your can size, your line, and your customer’s spec. Our standard 3104 coil is 0.2–3.0 mm, custom gauges on request; overall cold-rolled capability covers 0.2–3.8 mm. Send your drawing and target gauge and we’ll confirm what can be supplied for your order.
What widths and coil weights can you supply?
Finishing width 1200–2150 mm, hot-rolled width 1150–2150 mm, export coils up to 32 tonnes. Same caveat as above: those are overall capabilities, so confirm width, gauge, temper, tolerance, and coil weight for your order, and make sure your handling equipment can take the weight.
What is the difference between H19 and O temper?
H19 is extra-hard and strain-hardened, the usual D&I can body stock condition. O is fully annealed: softer, more formable, lower strength. They aren’t interchangeable. Confirm earing, surface finish, and ironing performance against the spec you agreed. If your process was qualified on one of them, don’t switch to the other without checking with your line engineers first.
What testing and certificates come with the coil?
Our factory is ISO 9001, ISO 14001 and ISO 45001 certified. Confirm mill certificate availability, test items, and format when you enquire.
What about MOQ and lead time?
Both are confirmed per order. Alloy, temper, gauge, width, and coil weight all feed into it, and lead time gets confirmed at the same time. Send your specification and we’ll confirm both in the quotation.
Talk to us before you specify
Send the buyer’s material specification or drawing with the required alloy, temper, thickness and tolerances. Include the width, coil weight and your line’s forming requirements so we can review the order against them.
Want to compare the two on your own line? Send your drawing, gauge, width, and temper. We’ll confirm whether a trial quantity is available. The right alloy is the one your line runs best on, and the fastest way to find out is to ask with the spec in hand.
See 3104 can body stock for the full specification, or contact us with your drawing.
Leave a Reply